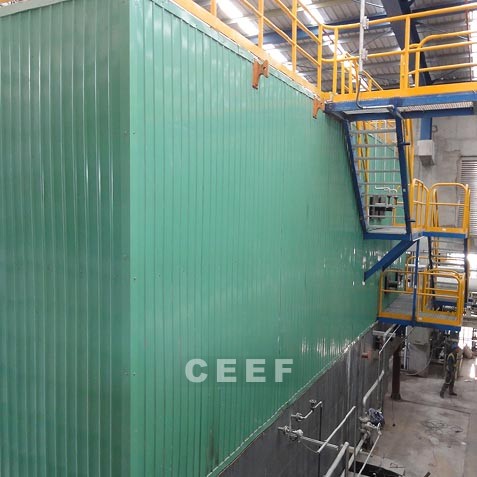
Product Overview
The coal-water slurry fired thermal fluid heater utilizes an advanced alternative liquid fuel—coal-water slurry—composed of finely ground coal, 27–35% water, and 1% chemical additives. This innovative fuel behaves like oil, allowing for pumpable transport and atomized combustion, achieving a combustion efficiency of over 90% (significantly higher than raw coal). By employing thermal oil as the heat carrier and forced liquid-phase circulation, the system delivers stable, high-temperature heat at low operating pressures. It is a clean, efficient, and cost-effective solution ideal for large-scale industrial heating, bridging the gap between coal economics and oil convenience.
Core Technical Features
- Energy-Saving Design: Highly efficient and energy-saving design philosophy.
- Optimized Structure: Optimized combustion chamber structure with a multi-radiation section.
- Maximized Absorption: Large radiation surface area for maximized heat absorption.
- Enhanced Transfer: Enhanced convective heat transfer technology.
- Ash Cleaning: Automatic and multi-directional ash cleaning systems.
- Temperature Control: Advanced throat and furnace exit flue gas temperature control.
- Maximum Safety: Automatic reset technology for explosion-proof doors ensuring maximum safety.
- Environmental Compliance: Complementary multi-stage dust removal and desulfurization technology for strict environmental compliance.
- Waste Heat Recovery: Integrated waste heat recovery systems.
- Automated Control: Highly automated combustion control and optimized system configuration.