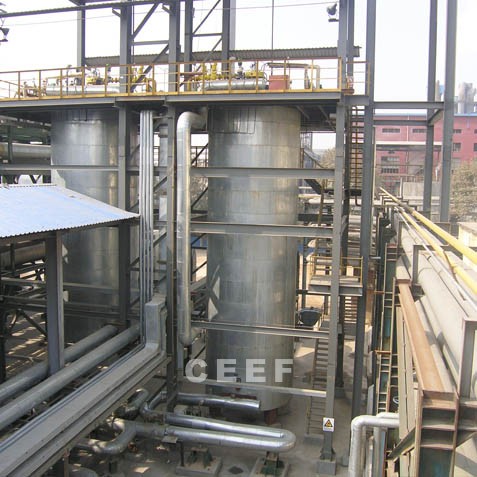
Product Overview
Engineered for ultimate reliability, the Dual-Fuel Thermal Fluid Heater is an advanced industrial heating system designed for optimal efficiency and maximum safety.
Core Technical Features
- Overload Heating Optimization: Specifically designed to safely handle peak capacity demands without compromising stability.
- Advanced Coil Structure: Features a dual-layer or multi-layer radiant coil design combined with a top-roof coil for maximized heat absorption.
- Enhanced Heat Transfer: Space thermal intensity optimization paired with strengthened convective heat transfer technology ensures superior thermal efficiency.
- Quick-Open Door Design: Innovative furnace structure allowing for rapid inspection, drastically reducing maintenance downtime.
- Auto-Reset Explosion Doors: State-of-the-art safety mechanisms that automatically reset after pressure release, protecting personnel and equipment.
- Automated Control System: Intelligent PLC-based controls for precision temperature management and operational ease.
- Eco-Friendly Low-NOx Combustion: Advanced burner technology ensuring strict environmental compliance and reduced emissions.
- Maximized Thermal Insulation: Reinforced insulation techniques to minimize heat loss and maximize overall thermal efficiency.